How to Choose a Low-Volume PCB Assembly Partner
Direct answer: Choose a low-volume PCB assembly partner by testing how the team controls revisions, sourcing approvals, first-article decisions, inspection, test, failures, and repeat builds. An equipment list matters only after the supplier demonstrates fit for the actual board and project stage.
What decision does this guide support?
This scorecard helps hardware teams compare suppliers for revision-sensitive, controlled-volume work. It turns sales claims into project-specific questions and observable records.
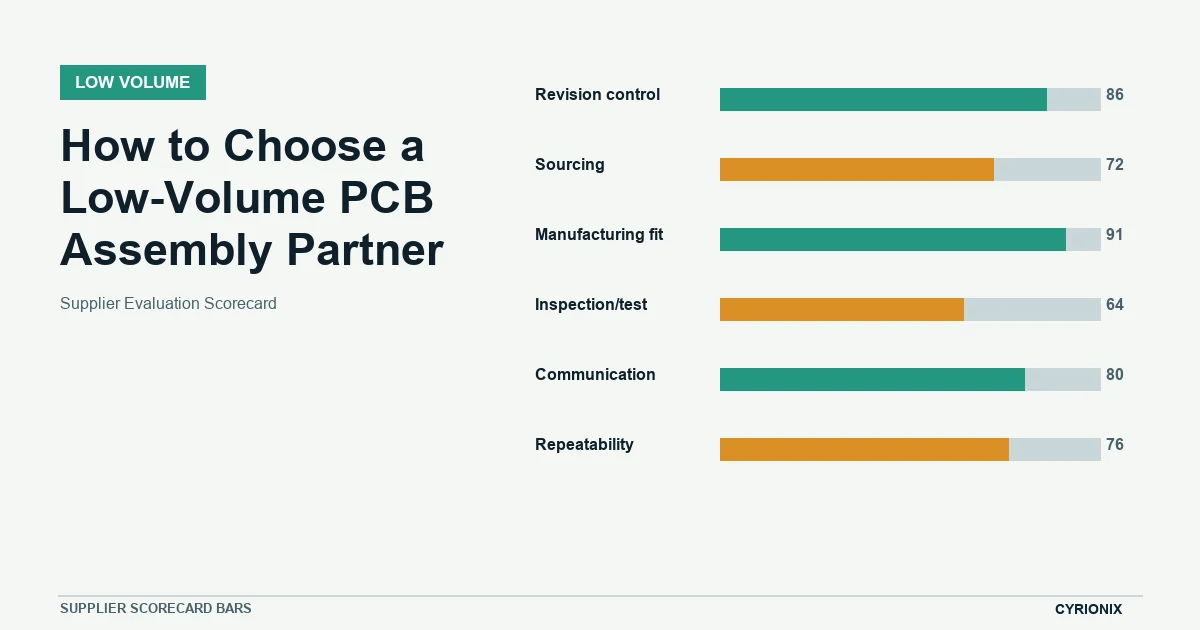
Supplier Evaluation Scorecard
Score the evidence behind each answer, not the confidence of the answer itself. Treat missing ownership, undocumented substitutions, and generic capability claims as decision risks.
| Evaluation area | Strong evidence | Red flag / hold condition |
|---|---|---|
| Revision control | Score how baselines, changes, substitutions, and batch identity are controlled. | Answers rely on informal memory. |
| Sourcing | Score traceability, quote assumptions, alternates, excess material, and escalation. | Substitutions can occur without approval. |
| Manufacturing fit | Request project-specific evidence for package, board, and process challenges. | Capability is asserted only through a generic equipment list. |
| Inspection/test | Score coverage definition, acceptance criteria, data, and failure handling. | Testing has no documented scope. |
| Communication | Score response ownership, issue format, decision deadlines, and time-zone handoff. | Problems are reported without an owner or recommended action. |
| Repeatability | Score records, feedback, setup reuse, and next-batch learning transfer. | A repeat order would restart from zero context. |
Define the project stage
Explain whether the build is intended to prove assembly, validate the design, support field trials, or establish a repeat process. A suitable partner should explain how that stage changes review depth, setup, and reporting.
Engineering-change handling
Ask how revisions and variants are identified, how superseded packages are blocked, and how mid-build changes are contained. The answer should include an effective-batch rule and a recoverable approval record.
Sourcing and alternates
Review source traceability, shortage escalation, excess material, and alternate approval. A credible process distinguishes purchasing execution from the customer engineering decision required for functional substitutions.
Inspection and test planning
Request proposed inspection and test coverage for the board, including evidence, acceptance limits, and failed-unit disposition. Generic references to AOI or testing do not define what will actually be checked.
Communication and repeatability
Evaluate who owns technical questions, how issues are formatted, and when a decision is escalated across time zones. Repeat orders should reuse a controlled baseline and prior build feedback instead of restarting from email history.
Weighted scorecard
Weight revision control, sourcing, manufacturing fit, inspection and test, communication, and repeatability according to project risk. Record the evidence supporting each score so the selection can be reviewed after the first build.
Run the evaluation against a real board
- Share a representative package. Use actual constraints instead of a generic capability survey.
- Request sample records. Review issue, approval, traceability, and test-output formats.
- Score the response. Separate proven controls from statements that still require verification.
Related Cyrionix resources
Review the low-volume PCB assembly service and prototype-versus-low-volume guide before selecting the manufacturing route.